Introduction: The New Standard of Modern Industrial High‑Bay Lighting
The Pain Points of Traditional Industrial Lighting Systems
Industrial and commercial high‑ceiling environments, including manufacturing workshops, logistics warehouses, large exhibition halls, indoor stadiums, and supermarket high‑bay areas, have long suffered from outdated lighting system limitations. Traditional high‑bay lighting solutions, such as metal halide lamps, high‑pressure sodium lamps, and early‑generation LED fixtures, present prominent operational drawbacks that increase enterprise operating costs and reduce workspace efficiency. These conventional products feature short service lifespans, severe luminous attenuation, unstable luminous output, and poor environmental adaptability. Most ordinary industrial lamps lack professional dustproof and waterproof structures, making them prone to dust accumulation, internal circuit oxidation, and water mist erosion in dusty, humid, and multi‑vibration industrial scenarios. The frequent failure of lighting equipment leads to high maintenance labor costs, frequent replacement expenses, and intermittent production interruptions, severely hindering standardized industrial operation.
In addition, traditional high‑bay lights operate in a fixed power mode throughout their service cycle, lacking intelligent induction and energy‑saving control functions. For large‑scale warehouses and intermittent working workshops with low personnel mobility, long‑term full‑power lighting causes massive unnecessary energy waste. The single luminous parameter setting also fails to meet the differentiated lighting demands of different production processes and working areas, resulting in mismatched lighting effects and actual usage scenarios. These long‑standing industry pain points urgently require upgraded, high‑durability, intelligent, and multi‑functional industrial lighting solutions to reshape the industrial lighting ecosystem.
Core Advantages of IP65 Heavy‑Duty UFO High Bay Lights
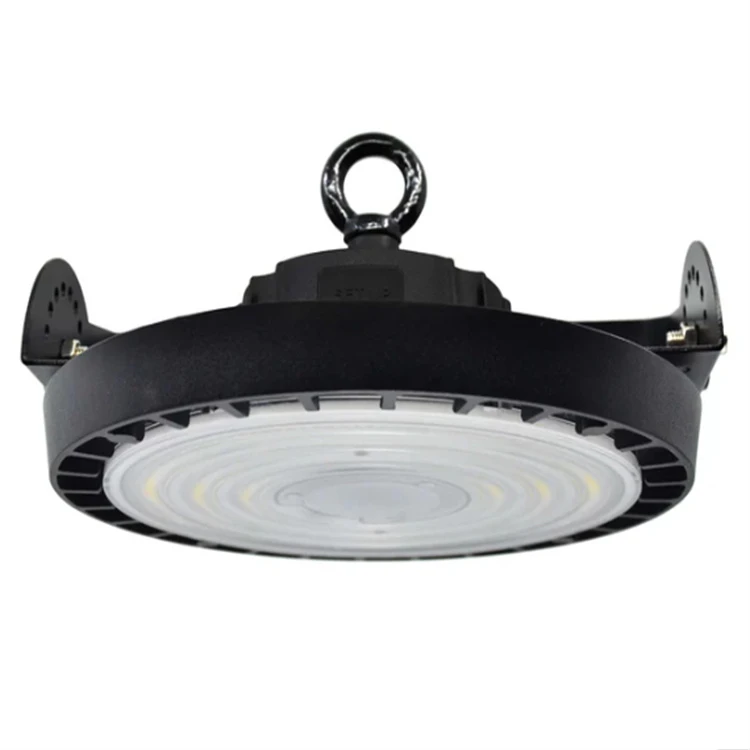
The IP65 heavy‑duty UFO LED high bay light is a newly upgraded industrial lighting fixture tailored for harsh industrial environments and intelligent energy‑saving lighting needs. Integrating industrial‑grade IP65 full protection performance, optimized UFO aerodynamic heat dissipation structure, long‑life light source system, and optional microwave intelligent induction module, this product perfectly solves the multiple defects of traditional high‑bay lights. Different from ordinary commercial LED lamps that only focus on basic lighting functions, this heavy‑duty model takes environmental adaptability, long‑term operational stability, intelligent energy saving, and low maintenance cost as the core design concepts, achieving comprehensive breakthroughs in durability, flexibility, and intelligence.
Equipped with a detachable and upgradeable microwave sensor module, the product realizes human body/object motion induction and automatic light adjustment, filling the gap of intelligent control in traditional industrial lighting. Meanwhile, the professional IP65 dustproof and waterproof rating enables the fixture to operate stably in complex and harsh industrial environments for a long time, greatly extending the service life of the equipment and reducing the overall operational cost of enterprise lighting systems. This paper will conduct an in‑depth professional analysis of the product's protective performance, structural design, luminous performance, intelligent induction function, and practical application value, providing a professional purchasing reference for industrial engineering contractors, facility managers, and enterprise procurement personnel.
In‑Depth Interpretation of IP65 Industrial‑Grade Heavy‑Duty Protection Performance
Definition and Industrial Standard of IP65 Protection Rating
The IP rating (Ingress Protection) is an international standard formulated by the International Electrotechnical Commission (IEC 60529), which is used to grade the dustproof, waterproof, and anti‑foreign‑object penetration capabilities of electrical equipment shells. The two digits of the IP rating represent solid particle protection level and liquid penetration protection level respectively, and IP65 is a high‑level industrial protection standard specially customized for heavy‑duty working scenarios. The first digit "6" means complete dust‑tight protection, with zero dust ingress into the lamp interior, completely isolating fine industrial dust, metal powder, and particulate impurities in the working environment from the core circuit and light source components. The second digit "5" represents anti‑low‑pressure water jet protection, which can resist water jet impact from any direction without water penetration and damage to internal components.
In the field of industrial lighting, IP65 is recognized as the minimum reliable protection standard for long‑term operation in harsh environments, far exceeding the IP20 and IP40 protection levels of ordinary indoor commercial lamps. Ordinary indoor lamps can only adapt to clean and dry office environments, and will quickly fail, age, or even short‑circuit and burn out in dusty and humid industrial workshops. In contrast, the IP65 heavy‑duty UFO high bay light fully complies with industrial protection specifications, realizing all‑round environmental isolation of the lamp body and providing a solid guarantee for long‑term stable operation of lighting equipment in complex scenarios.
Full‑Body Sealed Structural Design for Harsh Environment Adaptation
This UFO high bay light adopts a one‑piece die‑cast aluminum alloy housing, which is formed by high‑pressure die‑casting process at one time, with no splicing gaps in the whole lamp body. Compared with the split assembled structure of ordinary high‑bay lights, the integrated housing completely eliminates the hidden danger of dust and water penetration caused by loose assembly gaps. The high‑strength aluminum alloy material not only has excellent compression resistance, impact resistance, and deformation resistance, but also features outstanding anti‑corrosion and anti‑oxidation properties, which can resist the erosion of industrial humid air, weak acid and weak alkali gas, and oil fume in the working environment, avoiding shell rust, aging and damage.
The surface of the lamp body is treated with high‑temperature electrostatic spraying technology, which enhances the wear resistance and weather resistance of the housing. It can maintain a complete and stable protective structure for a long time even in scenarios such as mechanical vibration, forklift collision, and frequent environmental cleaning, ensuring that the IP65 protection performance does not decline with the extension of service time.
To achieve standard IP65 full protection, the product is equipped with high‑temperature resistant silicone sealing rings at all assembly gaps of the lamp body, including the connection between the light source panel and the housing, the driver installation cavity, and the sensor reserved interface. The silicone material has excellent elasticity, aging resistance, and high and low temperature resistance, which can maintain a tight sealing state in the temperature range of ‑20℃ to 60℃, avoiding sealing failure caused by thermal expansion and contraction of the lamp body.
The high‑transmittance PC light lens adopts integral compression sealing technology, which not only ensures high light transmittance and anti‑yellowing performance, but also prevents water mist and dust from entering the lamp body from the light outlet. The reserved microwave sensor installation interface is equipped with a special waterproof rubber plug, which can keep the sealing performance intact when the sensor is not installed, and can be quickly disassembled and upgraded without damaging the original protective structure after installing the sensor, realizing flexible switching of protection performance and intelligent functions.
Practical Value of IP65 Protection in Industrial Scenarios
In actual industrial operation scenarios, the IP65 protection performance brings tangible economic benefits and operational stability to enterprises. For dusty manufacturing workshops such as hardware processing, wood processing, and textile factories, the full dust‑tight design prevents dust from covering the LED light source and driver, avoiding luminous attenuation, light dimming, and circuit short circuit failures caused by dust accumulation. For humid environments such as food processing workshops, pharmaceutical factories, and cold storage warehouses, the water jet resistance function can cope with daily equipment water washing and environmental cleaning, preventing water mist and cleaning water from penetrating into the lamp body to damage electronic components.
More importantly, the stable IP65 protection performance effectively reduces the failure rate of lighting equipment. Traditional low‑protection lamps need frequent dust cleaning and maintenance, and the replacement cycle is short, resulting in continuous high maintenance costs. This IP65 heavy‑duty high bay light can operate continuously and stably in harsh environments for many years with almost no daily maintenance, greatly saving enterprise manpower and material resource costs, and improving the overall operational efficiency of industrial lighting systems.
Optional Microwave Sensor Module: Core Intelligent Energy‑Saving Upgrade
Technical Advantages of Microwave Induction Compared with Traditional Induction Modes
Most traditional intelligent induction lamps on the market adopt PIR infrared induction technology, which relies on human body heat radiation to realize induction lighting. This technology has obvious limitations in industrial high‑bay scenarios. PIR infrared induction is easily affected by environmental temperature, shelter obstacles, and personnel activity amplitude. In high‑ceiling installation environments (6‑15 meters high), the induction sensitivity is greatly reduced, and it cannot effectively detect personnel walking in warehouse aisles blocked by goods shelves, resulting in delayed lighting or failure to trigger lighting, which affects work safety. In addition, infrared induction cannot detect non‑heat‑generating moving objects such as automated handling robots and forklifts, which cannot meet the lighting needs of modern intelligent factories.
The optional microwave sensor module of this UFO high bay light adopts 5.8GHz high‑frequency microwave induction technology, which has comprehensive technical advantages over PIR infrared induction. Microwave induction detects moving objects through electromagnetic wave penetration scanning, which is not affected by environmental temperature, light intensity, and object temperature. It can penetrate non‑metal obstacles such as wooden shelves, plastic packaging, and wall partitions to sense moving personnel and equipment in advance, with a longer induction distance and higher sensitivity, fully adapting to high‑ceiling and multi‑obstacle industrial warehouse scenarios.
Core Functions and Working Principle of Microwave Sensor Module
The matched microwave sensor module has multi‑gear adjustable induction sensitivity, delay time, and dimming parameters, which can be customized according to on‑site working conditions. When the sensor detects moving personnel, forklifts, or handling equipment in the induction area, it will immediately trigger the lamp to turn on full power, providing high‑brightness uniform lighting for the working area. When the staff leaves and no moving objects are detected within the set delay time, the system will automatically dim the light or turn off the lamp, avoiding long‑term idle lighting energy waste.
Different from the single on‑off mode of ordinary induction lamps, this module supports stepless dimming adjustment, which can set low‑power standby brightness according to enterprise needs. It not only ensures the basic lighting safety of the workshop and warehouse at night, but also maximizes energy saving, realizing the perfect balance between lighting safety and energy consumption control.
The microwave sensor of this product adopts a standardized reserved interface design, realizing tool‑free quick assembly and disassembly, which is the core advantage different from integrated intelligent lamps. Users can choose to install the sensor module according to actual project needs: for workshops with continuous working hours and no energy‑saving demand, they can retain the original high‑brightness fixed lighting mode; for warehouses, stairwells, and intermittent working areas with low personnel mobility, they can install the microwave sensor to realize intelligent energy saving.
The modular upgrade design avoids the problem of fixed function of integrated lamps, reduces the difficulty of later equipment transformation, and improves the flexibility of product application. The sensor module also has independent IP65 waterproof and dustproof performance, which is consistent with the lamp body protection level, and will not reduce the overall environmental adaptability of the product after installation.
Economic Benefits of Microwave Intelligent Energy‑Saving System
For large industrial parks and logistics warehouse clusters, lighting energy consumption accounts for a high proportion of daily operational energy consumption. Traditional high‑bay lights work at full power for 24 hours, resulting in a large amount of invalid energy consumption in idle periods. After installing the optional microwave sensor module, the lamp can automatically identify the working state of the site, and the overall energy‑saving rate can reach 30%‑60% according to different usage scenarios. For enterprises with large‑area high‑bay lighting needs, it can save tens of thousands of yuan in electricity costs every year, and the economic benefit is extremely significant.
In addition, intelligent induction lighting can effectively reduce the cumulative working hours of the lamp, reduce the luminous attenuation speed and component aging degree, further extend the overall service life of the lamp, and reduce the frequency of equipment replacement and maintenance. It forms a dual cost‑saving system of electricity cost and maintenance cost for enterprises, which is an indispensable intelligent upgrade solution for modern energy‑saving industrial lighting projects.
Overall Heavy‑Duty Performance Optimization of UFO High Bay Light
Advanced Cold‑Hot Zones Separation Heat Dissipation System
Heat dissipation performance is the core factor determining the service life and luminous stability of LED high‑bay lights. Most ordinary UFO high‑bay lights adopt a mixed heat dissipation structure of light source and driver, which makes the heat generated by the LED light source during operation directly transfer to the driver cavity, resulting in accelerated aging of the driver electronic components, frequent light flicker, and early failure of the lamp. This heavy‑duty product adopts a professional cold‑hot zones separation heat dissipation structure optimized by FEA thermal simulation technology, which completely separates the LED light source heat zone and the driver cooling zone.
The LED lamp bead board is closely attached to the radial die‑cast aluminum heat sink, which quickly conducts and dissipates the heat generated by the light source through the multi‑fin heat dissipation structure, forming a high‑efficiency heat dissipation cycle. The driver is placed in an independent closed cold zone, completely isolated from the high‑temperature heat source of the light source, avoiding thermal superposition damage to the driver. This structural design effectively controls the working temperature of the core components, ensures the long‑term stable operation of the circuit system, and greatly slows down the luminous attenuation speed.
Long Service Life and Stable Luminous Attenuation Control
This product adopts high‑quality industrial‑grade SMD LED light source chips, with high luminous efficiency, strong stability, and low attenuation characteristics. After professional optical testing and aging verification, the product's L70 lumen maintenance life reaches 50,000 hours, which means that after 50,000 hours of continuous operation, the lamp can still retain more than 70% of the initial luminous flux, far exceeding the service life standard of ordinary civilian LED high‑bay lights. Calculated according to the daily working hours of industrial lighting, the product can work stably for more than 8 years without replacement, realizing long‑term zero‑maintenance lighting.
Benefiting from the optimized heat dissipation system and high‑quality light source configuration, the product's luminous attenuation rate is controlled within an ultra‑low range, avoiding the problems of rapid light dimming and color deviation of traditional lamps after long‑term use. At the same time, the lamp supports three‑gear CCT adjustable function (4000K neutral white / 5000K pure white / 6000K cool white) and three‑gear power adjustable function (60%/80%/100%), which can freely adjust the brightness and color temperature according to the actual lighting needs of the production site, meeting the high‑precision lighting needs of different processes such as product inspection, precision processing, and daily operation.
Flexible Dual Installation Structure and Wide Voltage Adaptability
To adapt to different industrial installation environments, this heavy‑duty high bay light is equipped with dual installation solutions: top suspension hook installation and U‑shaped adjustable bracket installation. The suspension hook is suitable for high‑ceiling overhead suspension installation of warehouses and workshops, with simple operation and stable installation. The U‑shaped bracket supports wall mounting and beam mounting, and can adjust the lighting angle freely, realizing targeted lighting for local working areas, with strong installation flexibility and wide scene adaptability.
In terms of power supply performance, the product adopts a high‑stability constant‑current driver, supporting a wide industrial voltage range. It can resist the voltage fluctuation common in industrial power grids, maintain flicker‑free and stable luminous output, effectively protect the internal circuit system, and avoid equipment damage caused by power grid instability. It is suitable for various industrial power supply environments at home and abroad, with strong compatibility and stability.
Application Scenarios and Purchasing Value Analysis
Core Application Scenarios
Relying on IP65 heavy‑duty protection, optional microwave intelligent induction, long life, and high stability performance, this UFO high bay light covers almost all industrial and commercial high‑bay lighting scenarios. It is widely used in hardware processing workshops, electronic manufacturing factories, textile factories, food processing plants, humid and dusty industrial production sites, large logistics warehouses, storage centers, indoor stadiums, exhibition halls, large supermarket shopping malls, and other high‑ceiling large‑space lighting scenarios. Whether it is a 24‑hour continuous production workshop or an intermittent idle warehouse, it can provide matched professional lighting solutions.
Comprehensive Purchasing Advantages for Industrial Users
Although high‑quality industrial‑grade high‑bay lights have a slight advantage in initial purchase cost compared with low‑end ordinary lamps, they have extremely low long‑term operational comprehensive costs. The IP65 high protection performance avoids frequent equipment failure and maintenance; the 50000‑hour long service life reduces replacement frequency; the optional microwave sensor realizes intelligent energy saving and reduces electricity expenditure. For long‑term operating industrial enterprises, the overall cost can be saved by more than 40% within three years, with extremely high cost performance.
The product's modular design enables it to have strong later upgrade potential. Users can freely match microwave sensors, dimming drivers, and other functional modules according to the upgrading of factory intelligent lighting systems, without replacing the whole lamp. It avoids the waste of repeated investment caused by equipment elimination, and realizes the iterative upgrade of lighting system with low cost, which is in line with the development trend of modern intelligent industrial lighting.
The flicker‑free high‑brightness uniform lighting effect effectively improves the working visibility of employees, reduces visual fatigue, and avoids operational safety hazards caused by insufficient lighting or uneven light. The industrial‑grade anti‑corrosion, waterproof and dustproof performance ensures the safe operation of electrical equipment in harsh environments, eliminating potential safety hazards such as short circuit and electric leakage caused by equipment damage, and providing a solid safety guarantee for industrial production and operation.
Conclusion
The IP65 Heavy‑Duty UFO High Bay Light With Optional Microwave Sensor is a new generation of high‑performance industrial lighting fixtures tailored for harsh industrial environments and intelligent energy‑saving needs. Its core competitive advantages are reflected in three dimensions: industrial‑grade IP65 full dustproof and waterproof heavy‑duty protection, upgradeable microwave intelligent induction energy‑saving system, and long‑life low‑attenuation professional luminous performance. Different from traditional single‑function industrial lamps, this product realizes the organic integration of durability, stability, intelligence, and flexibility, perfectly solving the pain points of short service life, poor environmental adaptability, high energy consumption, and difficult maintenance of traditional industrial lighting.
The cold‑hot zones separation heat dissipation structure ensures long‑term stable operation of the lamp, the L70 50000‑hour ultra‑long service life reduces enterprise maintenance costs, the dual installation design improves scene adaptability, and the optional microwave sensor module brings significant energy‑saving benefits. For industrial enterprises, engineering contractors, and facility managers, this product is a high‑cost‑performance, long‑term reliable, and upgradable professional industrial lighting solution. It can effectively optimize the enterprise lighting system, reduce operational energy consumption and maintenance costs, improve workspace lighting quality and operational safety, and is the preferred upgraded product for modern industrial high‑bay lighting projects.

How To Cooperate With Us?
We are happy to have total control over the manufacturing process and the calibre of our products since we have our own facilities. Since we are producers rather than just brokers, we are dedicated to providing our customers with the best pricing. Since we are certain that the price and quality of our products are clear, we invite customers to see our samples first. Our commitment to quality and customer satisfaction drives us to continuously provide top-notch goods.
Our address
3rd Floor, 5th Building, Hebei Industrial Park, Hualian Community, Longhua District, Shenzhen, China