Introduction: The Hidden Risks of Unprotected Industrial LED Lighting
Unique Environmental Challenges of Industrial Lighting Scenarios
Industrial lighting environments, covering cold storage warehouses, wet processing workshops, car wash stations, livestock breeding farms, agricultural greenhouses, and open industrial corridors, pose rigorous and long-term challenges to lighting equipment. Unlike indoor office lighting with constant temperature, dry air, and clean environment, industrial scenarios are characterized by three core destructive factors. First, pervasive particulate pollution including industrial dust, metal powder, feed dust, and floating granular impurities, which easily penetrate the interior of unenclosed lighting fixtures. Second, continuous moisture interference, including high ambient humidity, splashing water, condensed water vapor, and frequent water flushing, leading to internal dampness and electrical leakage risks. Third, dynamic temperature cycling, with long-term low-temperature environments in cold storage and high-temperature heat accumulation in closed workshops, accelerating the aging of lamp internal components.
These harsh environmental factors do not cause instantaneous failure of lighting equipment but trigger cumulative damage, forming hidden dangers for the long-term stable operation of the entire lighting system. Most standard LED tubes on the market only support IP20 or IP40 protection, designed for clean and dry indoor environments. When applied to industrial sites, their open structural design cannot resist external environmental erosion, resulting in a series of operational problems that restrict production efficiency and increase enterprise operating costs.
Common Failures of Low-Protection Industrial LED Lighting Systems
Long-term application practice verifies that low-protection LED tube lights will produce systematic failure problems under industrial harsh conditions, which are mainly reflected in four aspects. Firstly, dust accumulation causes luminous efficiency attenuation. Dust particles invade the lamp interior and adhere to LED chips and light guide plates, blocking light output and reducing effective luminous flux, resulting in dark lighting areas and uneven illumination in the workshop. Secondly, moisture intrusion leads to electrical failure. Water vapor and splashing water penetrate the lamp body, causing circuit board dampness, short circuit, and component burnout, leading to sudden lamp extinction and even potential safety hazards such as electric leakage.
Thirdly, accelerated component aging shortens service life. Humid and dusty environments accelerate the oxidation of internal circuits, the aging of welding points, and the attenuation of LED chip performance, making the actual service life of ordinary LED tubes far lower than the nominal value. Fourthly, frequent failure increases maintenance costs. Unprotected lighting equipment requires frequent inspection, replacement, and cleaning, consuming a large amount of labor costs and causing production downtime losses during maintenance. These pain points fully reflect that ordinary low-protection LED lighting cannot meet the sustainable operation needs of industrial systems, and high-level ingress protection represented by IP66 has become a necessary solution to break the industrial lighting dilemma.

Technical Definition and Core Standards of IP66 Ingress Protection Rating
IEC Standard Classification of IP Rating System
The IP (Ingress Protection) rating is a global unified electrical equipment protection standard formulated by the International Electrotechnical Commission (IEC 60529), which is used to quantitatively evaluate the ability of electrical equipment casings to resist solid particle intrusion and liquid penetration. The rating consists of two core digits, with the first digit representing solid dust protection level and the second digit representing liquid water protection level. The higher the digit value, the stronger the environmental resistance of the equipment.
In the industrial lighting field, the common protection grades include IP20, IP40, IP54, IP65, and IP66. Most civilian LED tubes adopt IP20/IP40 grades, which can only prevent large foreign objects such as fingers from entering and have no dust and water resistance. IP54 is a basic industrial protection grade, achieving dust-proof and splash-proof effects but unable to resist high-pressure water flushing and comprehensive dust penetration. As a high-standard industrial protection grade, IP66 realizes dual full-level protection of solid dust and liquid water, which is the core technical threshold for distinguishing civilian lighting and heavy-duty industrial lighting equipment.
Core Technical Parameters of IP66 Dust-Proof Performance
The first digit "6" of IP66 represents the highest-level solid protection standard in the IP rating system, namely complete dust-tight performance. Technically, the IP66-rated lamp body adopts an all-round sealed structural design, with no gaps or breathable holes in the casing, end caps, and wiring parts. This structure can completely block all types of solid particles in the industrial environment, including fine industrial dust, metal powder, pollen, feed particles, and tiny floating impurities.
Different from IP54 dust-proof design that only limits dust accumulation, IP66 protection achieves zero dust intrusion. No fine particles can penetrate the lamp interior to contact LED chips, drive circuits, and welding components. This fundamentally avoids luminous attenuation and circuit failure caused by dust accumulation, ensuring that the internal luminous structure and electrical system of the LED tube remain clean for a long time in dusty industrial environments, and maintaining stable luminous efficiency and electrical performance throughout the service cycle.
Core Technical Parameters of IP66 Water-Proof Performance
The second digit "6" of IP66 represents powerful high-pressure water jet resistance, which is the key technical advantage adapting to wet industrial scenarios. The IP66 protection standard strictly stipulates that the equipment can withstand high-pressure water jet flushing from any angle without liquid penetration and internal damage. Specifically, the lamp body can resist 100L/min high-flow water spraying, adapting to daily equipment flushing, site cleaning, rainwater splashing, and long-term high-humidity environment erosion in industrial sites.
The IP66 waterproof design of industrial LED tubes adopts a multi-layer sealing system, including high-density rubber sealing rings for end caps, threaded waterproof locking connectors, and integrated sealed PC casing. The tethered dust-proof and waterproof protective caps configured at the wiring interface ensure that the unused serial ports can still maintain a fully sealed state, avoiding water vapor intrusion from the interface gap. This comprehensive waterproof structure enables the lamp to operate stably in fully wet environments such as car wash workshops, food processing workshops, and cold storage defrosting environments, eliminating short circuit and burnout risks caused by water penetration.
Core Operational Benefits of IP66 Protection for Industrial LED Tube Systems
Stabilize Luminous Performance and Reduce Long-Term Light Decay Loss
Light decay is the core factor affecting the long-term lighting effect of industrial LED systems, and environmental erosion is the primary inducement of accelerated light decay. Ordinary low-protection LED tubes are prone to dust accumulation on the chip surface and damp aging of the luminous medium, resulting in continuous decline in luminous flux, color temperature deviation, and blurred lighting brightness after 1-2 years of use, which seriously affects industrial operation visibility and site safety.
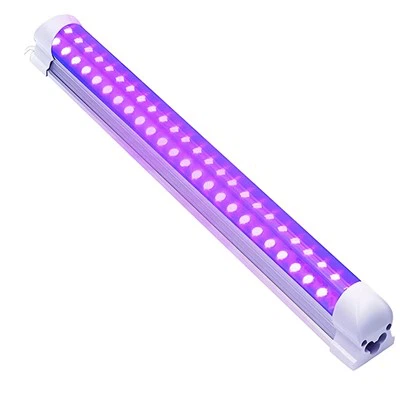
IP66 full-sealed protection fundamentally solves the environmental interference problem of the luminous system. The completely dust-tight structure ensures that the double-row high-density SMD LED chips inside the lamp are always in a clean and dry working environment, avoiding light blockage and heat dissipation obstruction caused by dust coverage. The high-pressure water-proof structure prevents condensed water vapor from adhering to the chip and circuit board, ensuring consistent heat dissipation efficiency of the lamp body. Stable and clean internal working conditions effectively inhibit luminous attenuation, making the long-term light decay rate of the LED tube far lower than that of ordinary products.
In actual industrial operation, the IP66-rated LED tube maintains more than 90% of the initial luminous flux after 30,000 hours of continuous operation, while ordinary IP40 LED tubes only retain 65%-70% of the luminous flux under the same working conditions. This excellent low-light-decay performance ensures the long-term uniformity and stability of industrial site lighting, avoids frequent brightness attenuation and dark area generation, and maintains standardized lighting conditions for industrial production, inspection, and operation.
Extend Service Lifespan and Reduce Equipment Replacement Frequency
The nominal service life of most ordinary industrial LED tubes is 30,000 hours, but affected by dust, moisture, and temperature changes, the actual effective service life is only 15,000-20,000 hours, with a failure rate as high as 30% within two years. Frequent lamp replacement not only increases equipment procurement costs but also causes intermittent lighting interruptions and affects continuous production operation.
IP66 protection cooperates with the optimized thermal management system and high-strength PC shell structure to greatly extend the effective service life of industrial LED tubes. The fully sealed structure isolates external corrosive media, prevents circuit oxidation and component aging, and ensures that LED chips and drive circuits operate within a stable temperature and humidity range. Coupled with the high-transmittance anti-aging PC casing and shock-resistant structural design, the lamp can resist vibration, temperature cycling, and environmental erosion for a long time.
The rated service life of IP66 industrial LED tubes reaches 50,000 hours of continuous operation, and the actual on-site service cycle can reach 4-6 years under industrial harsh conditions, which is 2-3 times that of ordinary low-protection LED tubes. The ultra-long service cycle greatly reduces the frequency of equipment replacement, eliminates production downtime losses caused by lamp failure replacement, and realizes long-term stable operation of the industrial lighting system.
Eliminate Electrical Safety Hazards and Improve System Operational Stability
Industrial lighting systems belong to long-term continuous operating electrical equipment, and electrical safety is the core guarantee of on-site production safety. Low-protection LED tubes have poor sealing performance, and water vapor and dust intrusion easily cause internal circuit dampness, short circuit, electric leakage, and even local burnout and sparking, which bring serious safety hazards to flammable and dusty industrial sites such as chemical workshops, grain warehouses, and breeding farms.
IP66 full-level dust and water protection completely isolates the contact between internal electrical components and external harsh media. The integrated sealed lamp body and insulated waterproof connectors have excellent insulation and anti-leakage performance, which can effectively prevent electric leakage, short circuit, and circuit burnout caused by water and dust intrusion. Even in the environment of high-pressure water flushing and long-term high humidity, the electrical system of the lamp remains stable and safe, with zero electric leakage risk.
In addition, the IP66 protection structure matches the industrial anti-vibration and anti-impact design, which can resist slight vibration generated by industrial mechanical operation and accidental impact during on-site operation, avoiding internal circuit disconnection and component damage. This all-round protection greatly improves the anti-fault ability of the industrial lighting system, realizes 24/7 uninterrupted stable operation, and eliminates safety accidents and system paralysis caused by lighting equipment failure.
Reduce Long-Term Operation and Maintenance Costs of Enterprises
The comprehensive cost of industrial lighting includes equipment procurement cost, installation cost, daily maintenance cost, replacement cost, and downtime loss cost. Although the initial procurement cost of IP66 high-protection LED tubes is slightly higher than that of ordinary products, it can bring significant cost reduction benefits in the whole life cycle, which is the core reason why more and more industrial enterprises choose to upgrade IP66 lighting systems.
In terms of maintenance costs, ordinary low-protection LED tubes require regular dust cleaning, damp inspection, and fault detection, consuming a lot of manual maintenance resources every year. While IP66 fully sealed tubes do not need daily dust and water cleaning maintenance, and the internal structure is permanently clean and stable, reducing daily maintenance labor costs by more than 80%. In terms of replacement costs, the ultra-long service life avoids frequent batch replacement of lamps, reducing the annual equipment renewal investment of enterprises.
More importantly, the stable operation of IP66 lighting systems eliminates production downtime losses caused by sudden lamp failure. For continuous production industrial enterprises, temporary lighting failure will lead to production suspension, operation delay, and product quality inspection errors, with huge invisible losses. IP66 protection ensures zero sudden failure of the lighting system, maintains continuous and stable production operation, and creates long-term economic benefits for enterprises.
Scenario Adaptability Advantages of IP66 Industrial LED Tube Lighting System
Low-Temperature Cold Storage and Freezer Warehouse Scenarios
Cold storage and freezer warehouses are typical high-humidity and low-temperature industrial environments, with long-term ambient temperature below 0℃ and air humidity close to saturation, prone to condensed water frosting and dust accumulation. Ordinary LED tubes are easy to frost and seep water internally in low-temperature and high-humidity environments, resulting in circuit failure and light decay acceleration.
IP66 fully sealed protection structure can resist low-temperature condensed water penetration and frost erosion, and the internal electrical components can operate stably in ultra-low temperature environments without damp failure. The high-density PC shell has excellent low-temperature resistance, no embrittlement and cracking in long-term low-temperature operation, ensuring structural integrity and lighting stability. It solves the pain points of short service life and frequent failure of traditional cold storage lighting, and is the most matching lighting solution for cold storage industrial scenarios.
Wet Workshop and Car Wash Flushing Scenarios
Food processing workshops, textile wet workshops, and car wash stations have frequent water flushing and splashing water, with complex and changeable on-site water environments. Ordinary lighting equipment cannot resist high-pressure water flushing, and water intrusion will cause rapid failure of the lamp body. The IP66 high-pressure water jet resistance standard fully adapts to frequent flushing operation needs, and the multi-layer sealed structure can withstand all-angle high-flow water spraying without water penetration.
At the same time, the dust-tight performance avoids the mixing of water stains and dust to form dirt accumulation inside the lamp, maintaining long-term high luminous efficiency. It realizes maintenance-free stable operation in long-term wet and flushing environments, greatly improving the durability of workshop lighting systems.
Agricultural Breeding and Greenhouse Industrial Scenarios
Livestock breeding farms and agricultural greenhouses have high air humidity, floating feed dust, fecal dust, and plant debris, and the environment contains trace corrosive gases. Ordinary LED tubes are prone to dust blockage and corrosive gas erosion, leading to rapid light decay and component aging.
IP66 full dust-proof structure completely isolates all kinds of agricultural floating dust, and the sealed casing resists the erosion of humid corrosive gases, protecting LED chips and drive circuits from chemical corrosion. The stable luminous output meets the long-term lighting needs of agricultural planting and breeding, improves the utilization rate of lighting equipment in agricultural industrial scenarios, and reduces the frequent replacement and maintenance troubles of agricultural lighting.
Open Industrial Corridor and Outdoor Shelter Scenarios
Covered outdoor industrial corridors, factory passageways, and outdoor sheltered working areas are affected by natural wind, dust, rainwater splashing, and day-night temperature difference alternation. Low-protection lighting equipment is easy to age and fail under natural environmental erosion. IP66 protection can resist outdoor dust invasion and rainwater splashing, adapt to temperature cycle changes, and maintain stable lighting performance in semi-outdoor industrial environments, realizing all-weather reliable lighting protection.
Comparative Analysis: IP66 LED Tube vs Ordinary Low-Protection Industrial Lighting
Performance Gap in Environmental Resistance
Ordinary IP20/IP40 LED tubes adopt open hollow structure, with no sealing treatment at the end caps and interfaces, unable to resist dust and water intrusion, and can only be used in dry and clean indoor environments. IP54 semi-protection products have basic splash-proof and dust-proof capabilities, but cannot resist high-pressure water flushing and comprehensive fine dust penetration, and will still have dust accumulation and water seepage failure after long-term use in industrial harsh environments.
IP66 industrial LED tubes adopt full-process integrated sealing technology, with sealed end caps, waterproof locking interfaces, and integral closed casings, realizing full coverage of dust and water protection. Whether it is fine industrial dust or high-pressure water jet, it can be completely isolated, and the environmental resistance is comprehensively upgraded, which is fundamentally different from ordinary low-protection lighting products in structural design and performance threshold.
Gap in Life Cycle and Loss Control
In the same industrial harsh environment, the average effective service life of ordinary low-protection LED tubes is only 1.5-2 years, with annual light decay rate as high as 15%-20%, and the lighting system needs large-scale maintenance and replacement every year. The IP66 high-protection LED tube has an average effective service life of 4-6 years, with annual light decay rate controlled below 5%, and the luminous performance remains stable for a long time.
In terms of comprehensive loss, ordinary lighting systems have high failure loss, light efficiency loss, and maintenance loss, with high annual comprehensive operating costs. IP66 protection effectively suppresses all kinds of environmental-induced losses, realizes low attenuation, low failure, and low maintenance of the lighting system, and has outstanding economic advantages in the whole life cycle.
Gap in System Safety and Stability
Low-protection lighting systems have hidden dangers such as electric leakage, short circuit, and local burnout in humid and dusty industrial environments, with poor operational stability and high failure rate. The IP66 protection system realizes full isolation of external environmental interference, with safe and stable electrical performance, no electric leakage risk, strong anti-fault ability, and can adapt to long-term uninterrupted industrial operation needs, greatly improving the overall safety and reliability of the industrial lighting system.
Conclusion: IP66 Protection Is the Core Upgrade of Modern Industrial Lighting Systems
Industrial lighting is an important basic supporting system for enterprise production and operation, and its stability, durability, and economy directly affect production efficiency, operation safety, and enterprise operating costs. Facing the harsh environmental challenges of industrial scenarios, ordinary low-protection LED lighting can no longer meet the needs of long-term stable and low-cost operation of modern industrial systems.
As a high-standard industrial protection configuration, IP66 rating brings multi-dimensional core value upgrades to industrial LED tube lighting systems. Its full dust-tight and high-pressure water-proof performance fundamentally solves the problems of dust accumulation, water intrusion, accelerated light decay, and premature failure of traditional lighting equipment. It effectively extends the service life of lighting equipment, stabilizes luminous performance, eliminates electrical safety hazards, and greatly reduces the long-term operation and maintenance costs of enterprises.
Whether it is low-temperature cold storage, wet processing workshops, agricultural breeding bases, or semi-outdoor industrial spaces, IP66 high-protection LED tubes can achieve scenario-adaptive stable operation, becoming the most cost-effective and reliable lighting solution for modern industrial sites. For industrial enterprises pursuing long-term stable operation and refined cost control, upgrading to IP66 protected industrial LED tube lighting systems is not only a performance upgrade of lighting equipment but also an important measure to optimize enterprise operation efficiency and reduce comprehensive operating costs, with significant practical application value and long-term economic benefits.

How To Cooperate With Us?
We are happy to have total control over the manufacturing process and the calibre of our products since we have our own facilities. Since we are producers rather than just brokers, we are dedicated to providing our customers with the best pricing. Since we are certain that the price and quality of our products are clear, we invite customers to see our samples first. Our commitment to quality and customer satisfaction drives us to continuously provide top-notch goods.
Our address
3rd Floor, 5th Building, Hebei Industrial Park, Hualian Community, Longhua District, Shenzhen, China